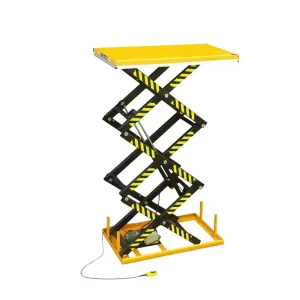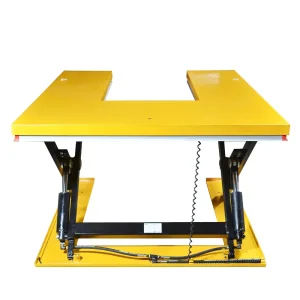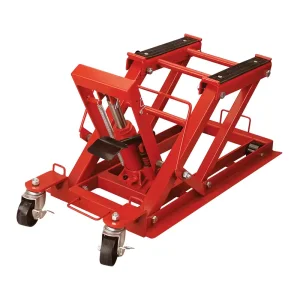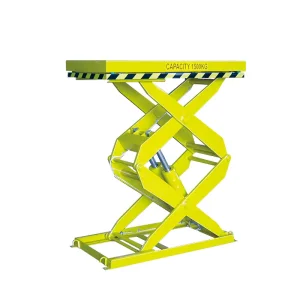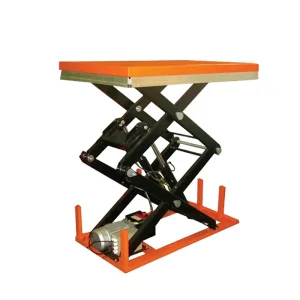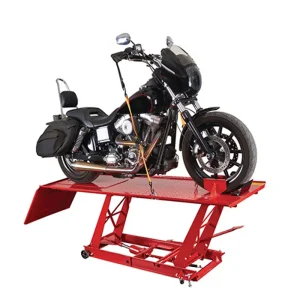
High-capacity stationary, low-profile, and multi-stage electro-hydraulic scissor lift platforms optimized for conveyor network integration.
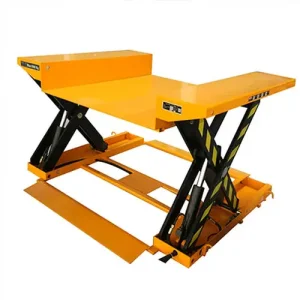
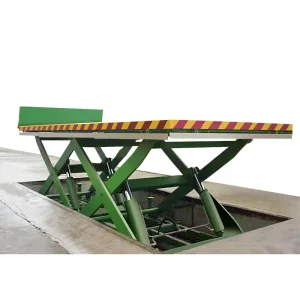
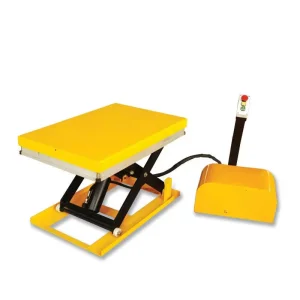
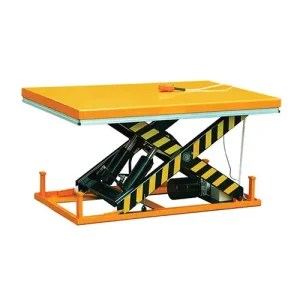
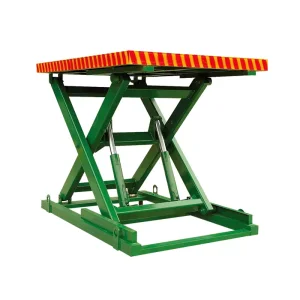
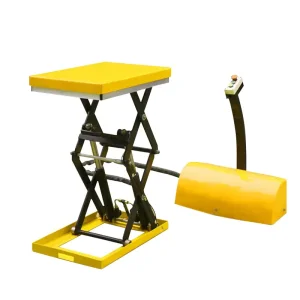
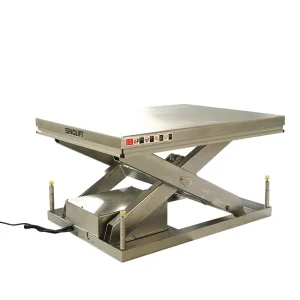
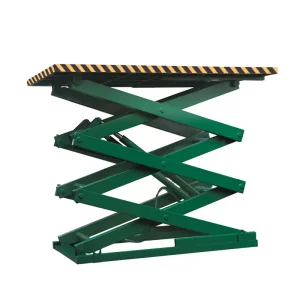
In modern industrial logistics, automated manufacturing, and smart warehousing, the integration of scissor lift conveyors represents a critical convergence of heavy-duty vertical positioning and horizontal linear transport. As global supply chains accelerate toward Industry 4.0 paradigms, the global market for hydraulic and electric scissor lift tables integrated with powered roller, belt, or chain conveyors has experienced unprecedented growth.
Historically, vertical lifting mechanisms and horizontal conveyor networks operated as isolated islands of automation. Today, international manufacturing facilities require continuous, real-time height compensation to bridge differences between multi-tier conveyor systems, automated guided vehicles (AGVs), autonomous mobile robots (AMRs), and ergonomic manual assembly stations. Key macro factors driving procurement across North America, Europe, and the Asia-Pacific region include:
Global procurement teams evaluating scissor lift conveyor suppliers and exporters face multifaceted challenges beyond mere price point considerations. Specifying a scissor lift platform for heavy continuous-duty integration requires rigorous mechanical and hydraulic risk assessment:
Structural Rigidity and Deflection Control: Under eccentric or off-center dynamic loads—common when heavy pallets enter a conveyor top from an adjacent line—lift tables experience torsional twisting. Premium manufacturers utilize high-tensile structural steel (such as Q345B or ST52-3) and solid steel scissor legs to restrict dynamic platform deflection within 0.05% of table length.
Hydraulic Valve Synchronization & Smooth Positioning: When paired with automated conveyors, vertical leveling accuracy is paramount. Advanced systems integrate proportional hydraulic valves or electro-servo motor drives coupled with absolute optical encoders, achieving repeatability tolerance under ±1.0mm. This precision prevents conveyor jam-ups and pallet structural damage during high-speed transfers.
Delivering world-class material handling equipment backed by rigorous standard testing and expansive manufacturing infrastructure.
Sinolift is one of the leading material handling equipment manufacturers in China and a key player in the Global hydraulic industry. Our headquarter, Shanghai Sinolift Mechanical and Electrical Equipment Co., Ltd. is located in Nanhui Industry Park and was established in 2005. From 2017, we invested in our third new plant in Hangzhou City, Zhejiang Province to manufacture specialized hydraulic handling equipment such as Dock Equipment, Tail lifts, Dock levelers, Lift Tables, and Access lifts.
All of our products are manufactured with the highest quality materials and we guarantee their total dependability. Whether your company is moving heavy-duty industrial materials or lightweight parts, Sinolift will have a customized materials handling solution tailored for the task. Each product is engineered and tested according to strict national and international standards including JB/T 9229.1(2/3)-1999. We have successfully passed ISO9001, CCMA, CE, and other authoritative international certifications.
Our high-performance products are exported to Europe, America, the Middle East, Southeast Asia, and over 120 other countries and regions worldwide. Domestically, our distribution network spans across all provinces with hundreds of authorized distributors, supporting a complete, rapid-response sales and after-sales service framework.
Contact Our Engineering Team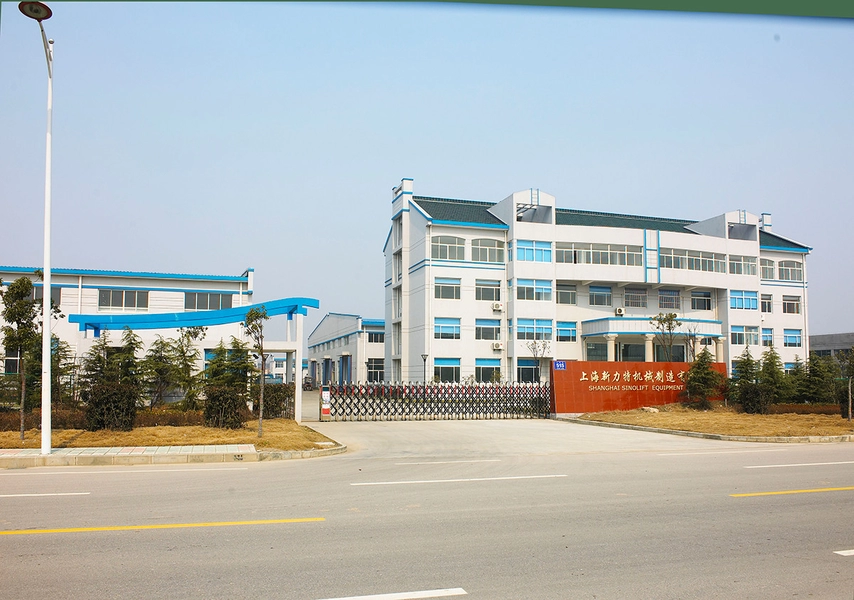
Why leading Fortune 500 companies and enterprise integrators select Sinolift for high-precision lifting conveyors.
Having over 5,000 successful installations worldwide has supplied us with the in-depth experience and practical technical knowledge that we pass on to every project that we handle, guaranteeing seamless engineering integration.
At SINOLIFT, we take pride in having the widest hydraulic handling product range available. We always make sure to have a minimum stock of 2,000+ units—a testament to our dedication to product availability ensuring fast delivery for urgent site requirements.
Our vast array of options guarantees that we can cater to all your material handling needs, no matter the specifics of your operation or the complexity of your requirements. You can be sure that SINOLIFT can provide the exact customized solution for your application.
Scissor lift conveyors are highly versatile capital assets utilized across diverse heavy industrial environments. By matching specific conveyor top module configurations—such as zero-pressure accumulation roller conveyors, heavy-duty chain conveyors, or multi-directional ball transfer tables—with tailored lifting power units, Sinolift delivers standardized and bespoke macro solutions:
In automated automotive manufacturing, precision engine and chassis mating lines rely on heavy-duty double-scissor or multi-scissor lift tables. Operating under continuous S1 electric motor regimes, these systems raise vehicle sub-assemblies to precise workstation heights while integrated motorized roller beds move payloads seamlessly along the line.
Logistics facilities operating 24/7 utilize Sinolift low-profile lift tables with belt conveyor tops to bridge height variations between automated main sorters and manual pallet loading stations. Built-in photo-electric sensors trigger dynamic automatic height adjustments as pallet stack heights increase, maintaining optimal ergonomic transfer geometry for workers.
For sanitary and wash-down applications, Sinolift manufactures 304 and 316 stainless steel scissor lift conveyors equipped with IP66-rated hydraulic power packs and food-grade hydraulic fluid. Designed to withstand harsh chemical sanitization, these units operate reliably in sub-zero freezer environments down to -30°C without fluid viscosity failure or structural embrittlement.
As industrial automation transforms toward fully autonomous smart factories, Sinolift remains at the forefront of lifting and conveyor engineering. Our product development roadmap focuses on four key pillars of technological innovation:
Next-generation Sinolift conveyor lifts feature embedded vibration, thermal, and hydraulic pressure sensors connected directly to facility SCADA or cloud-based maintenance dashboards. By monitoring pump pressure spikes, fluid degradation, and scissor bearing wear in real time, maintenance teams can schedule servicing proactively before costly unscheduled downtime occurs.
Replacing standard electro-hydraulic cylinders, high-precision applications can utilize heavy-duty electromechanical ball-screw actuators driven by servo motors. This provides ultra-precise vertical positioning within ±0.2mm, cleanroom-level oil-free operation, and significant energy savings via regenerative braking motor drives.
Our scissor lift conveyors now support integrated optical and digital CANbus communication interfaces to seamlessly exchange handshake signals with incoming Autonomous Mobile Robots (AMRs). Lifts align precisely with robot decks, ensuring zero misalignment during automated payload transfers.
Incorporating variable frequency drives (VFD) and smart power management units reduces power consumption by up to 35% during idle phases and low-duty cycles, assisting enterprise clients in achieving their global ESG carbon reduction targets.
Exporting industrial machinery globally demands rigorous adherence to regional regulatory frameworks and safety standards. Sinolift scissor lift conveyor systems are designed, tested, and certified to meet or exceed global engineering requirements:
In-depth answers to common engineering, purchasing, and integration queries regarding scissor lift conveyors.
Discover our comprehensive collection of triplex lifts, stainless steel platforms, double-scissor lifts, and specialized material elevators.